Services
Custom steel processing at the Hòa Khánh Industrial Park plant
Coil processing, levelling, cut-to-length, CNC profile cutting and sawing at our Hòa Khánh Industrial Park plant.
8 service groups
From steel coil to finished components
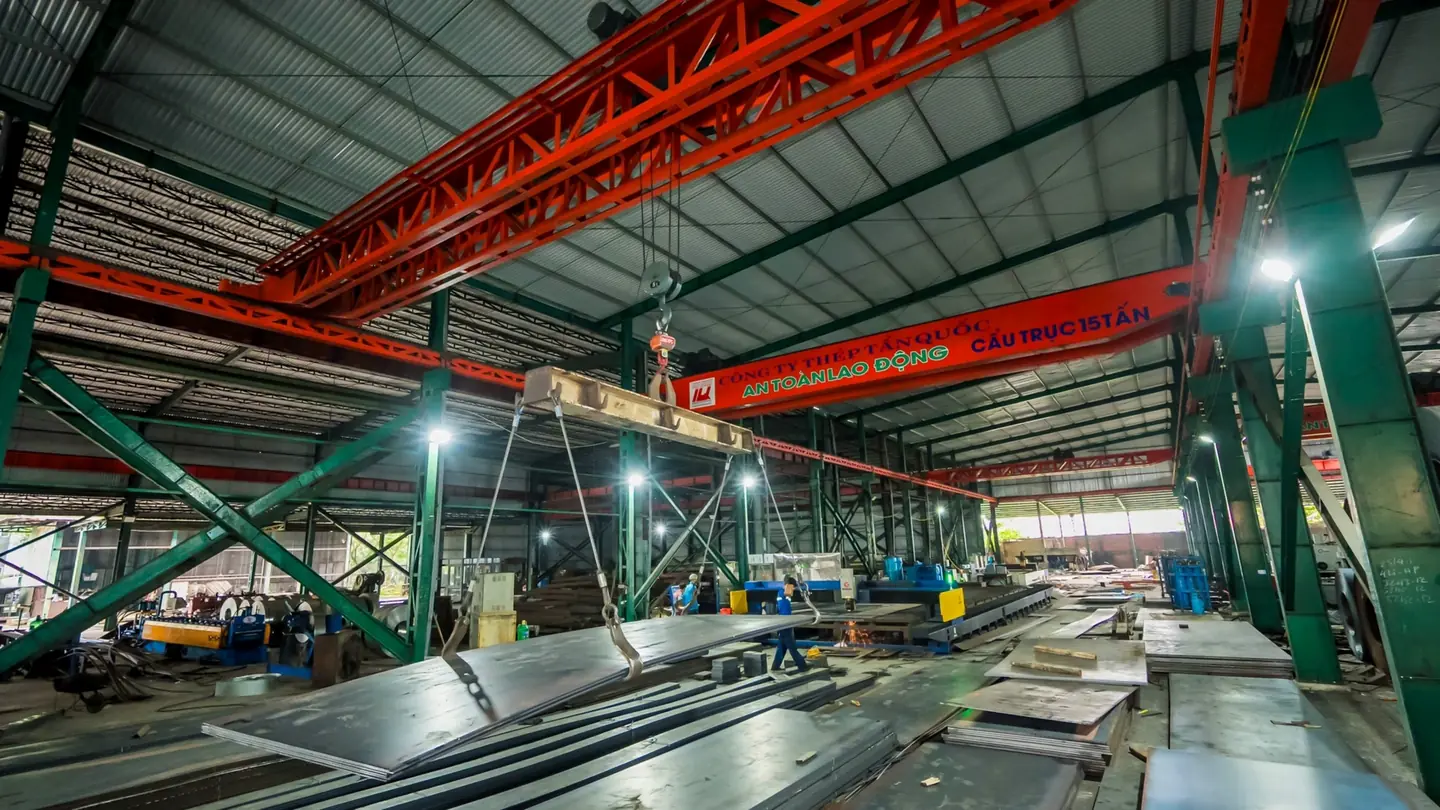
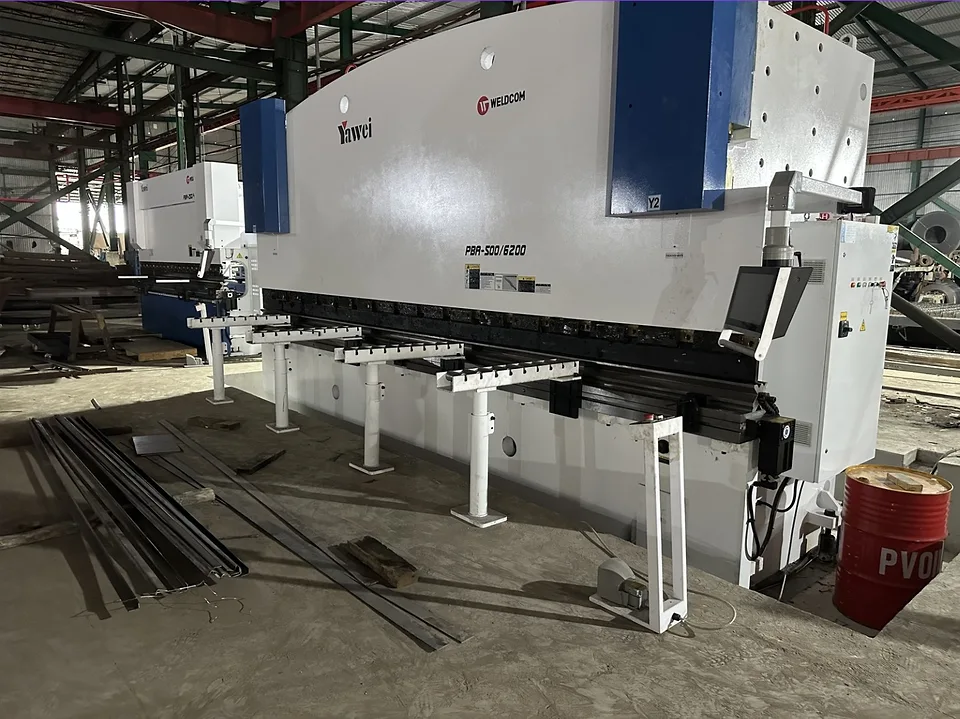
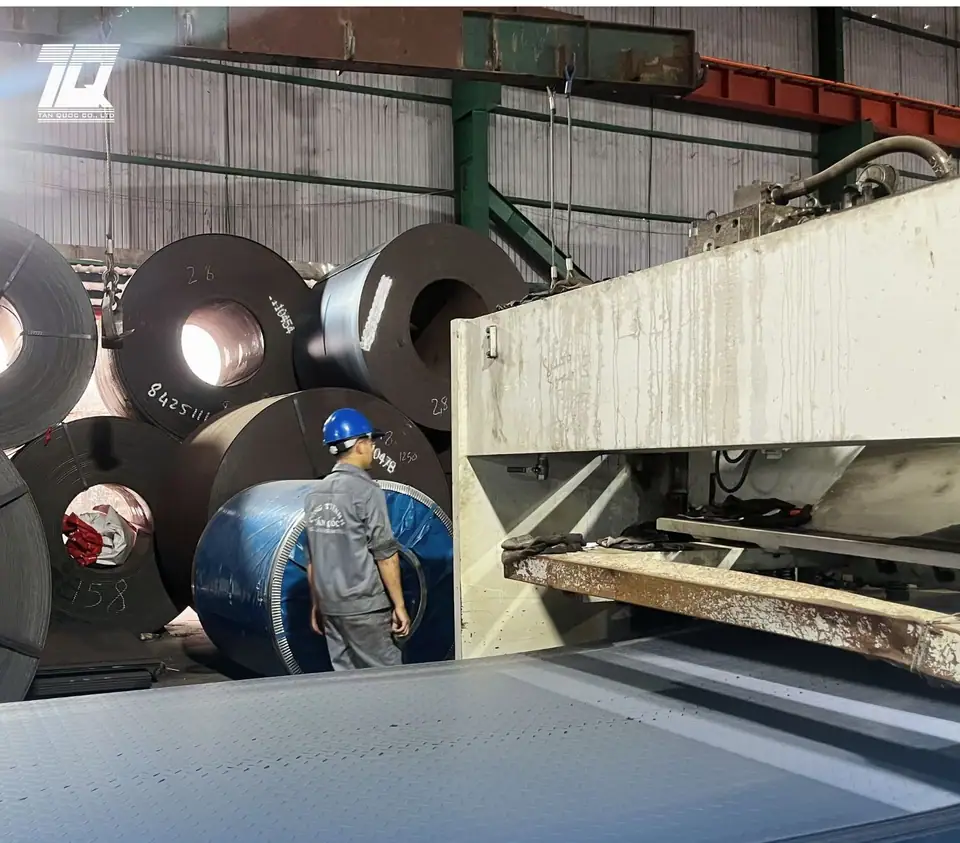
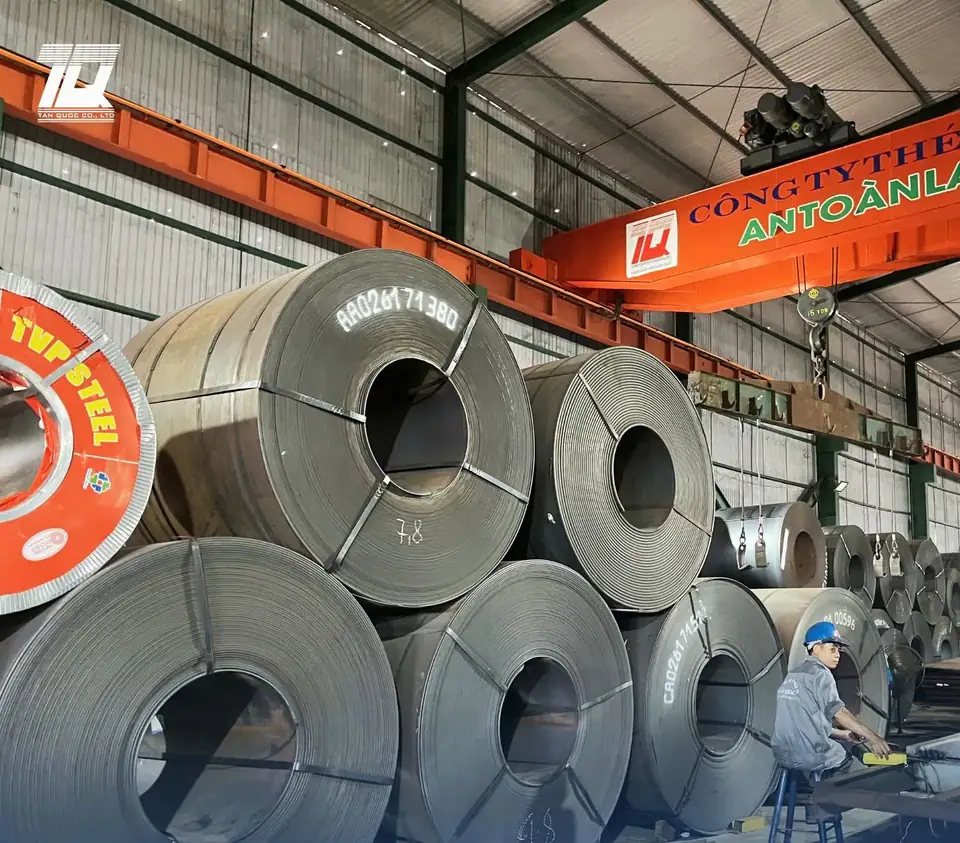
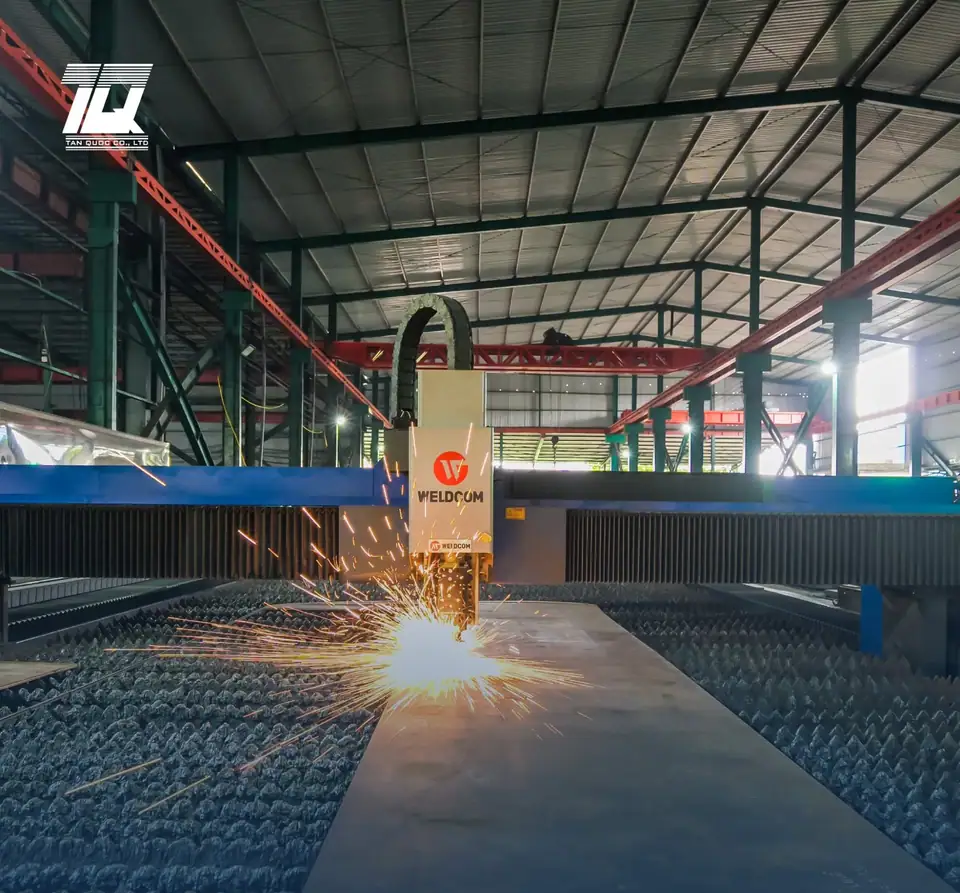
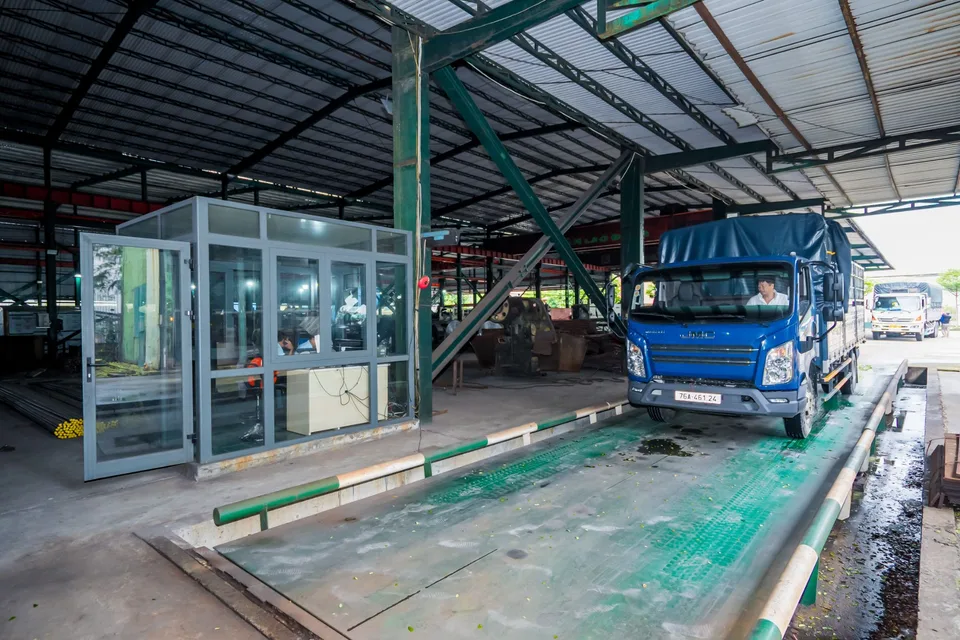
The Hòa Khánh plant has been equipped since 2005 with a 35-ton overhead crane, a coil processing line, CNC laser and plasma cutting machines, a 500-ton CNC hydraulic press brake spanning 6,200 mm and a structural fabrication shop. CNC cuts and shearing follow the drawings exactly; every lot is inspected by QC so mis-cuts are kept to a minimum. Cutting orders are scheduled immediately upon arrival – no long wait times. Choose a service group to see specific items; each group links to the matching steel specifications in the product catalogue. To see the shop floor first, read the photo tour inside the Tan Quoc workshop; to take off quantities before sending drawings, use the steel section, plate and pipe weight reference tables. Goods are delivered through our transport partners across our delivery coverage across 20 provinces.
 01
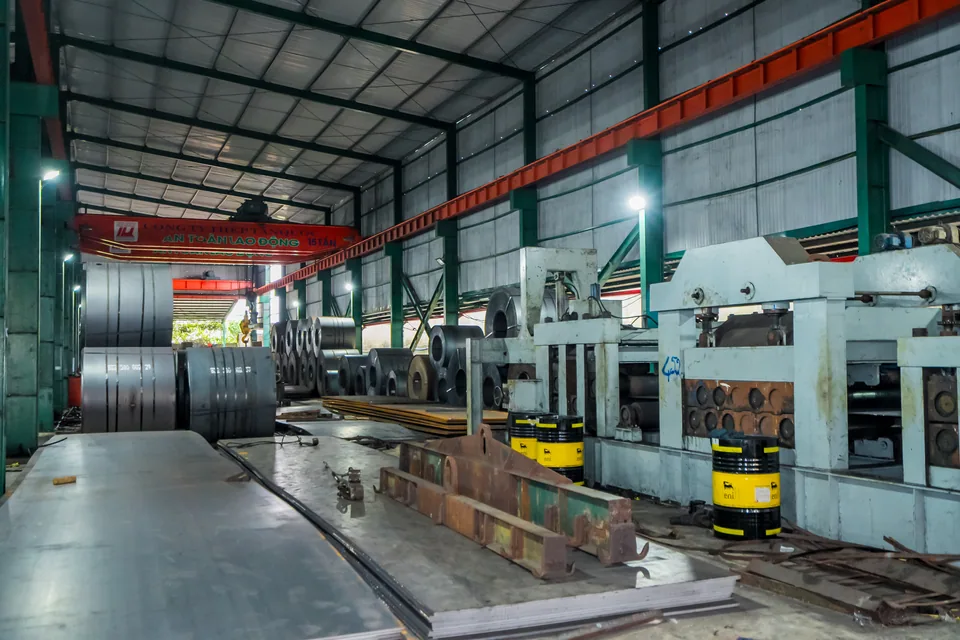
Coil processing/slitting
Hot-rolled coil processing line handling 1.2 – 23 mm thickness up to 1,500 mm width at the Hòa Khánh plant. Sheets exit flat with no warping, length tolerance ±2 mm.
- Coil slitting to width
- Cut-to-length from coil, 1 – 12 m
- Coil levelling
- Levelling, cutting and shearing to order
- Coil coating processing
Raw materials and related reading
Related materials
- CRC cold-rolled coil – thin coil 0.3 – 3.0 mm, 1000 – 1250 mm wide, for cut-to-length and slitting
- GI galvanized coil – Z80 – Z275 coating, processed into roofing sheet, purlins and ductwork
- GL aluminium-zinc coil – AZ70 – AZ150 for roofs, cladding and coastal purlins
- PPGI / PPGL pre-painted coil – full range of standard RAL colours, slit to width for roofing, cladding and panels
- EG electro-galvanized coil – thin, even 5 – 20 µm coating, cut to sheet for powder-coated electrical cabinets
- Terne-coated (lead-tin) coil – resists fuel and chemicals, cut to sheet for fuel tanks and fuel lines
- Chequered coil – decoiled and cut to the exact chequered-plate length required
- Stainless coil 201 / 304 / 316 – stainless coil 0.3 – 3.0 mm, slitting to width available
 02
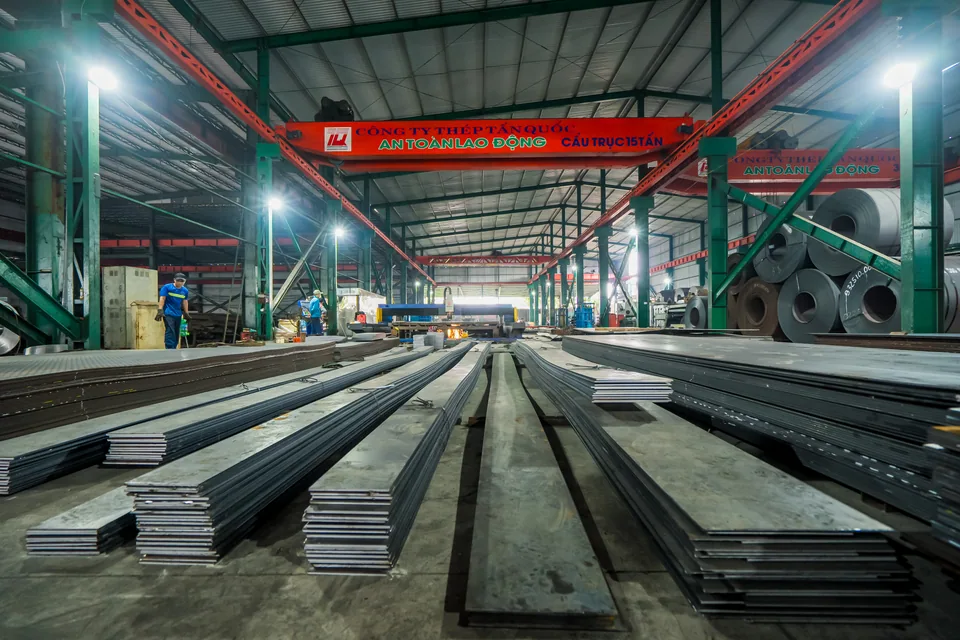
Steel plate processing
Gusset plates, base plates and flanges cut to drawing from SS400 / Q345 plate stock, 4 – 100 mm thick; surface renewal and polishing of warehouse inventory plate.
- Custom gusset plate fabrication
- Levelling, polishing and plate renewal
- Plate cutting to size
- Weld-edge bevelling
Raw materials and related reading
Related materials
- PO hot-rolled plate – pickled and oiled, so shot-blasting can be skipped before welding and painting
- Cold-rolled plate – 0.3 – 3.0 mm, smooth surface for stamped, bent and powder-coated parts
- Galvanized plate – 3 – 20 mm plate hot-dip galvanized after cutting to drawing
- Chequered plate – cut to size for platforms, stair treads and manhole covers
- C45 / S45C plate – 6 – 100 mm, cut blanks for machine bases, flanges and fixture plates
- 65G / 65Mn plate – wear-resistant spring steel, blanks for blades, screen plates and liners
- Shipbuilding plate AH36 / DH36 / EH36 – profile cutting and weld bevelling for hulls, barges and wharf structures
 03
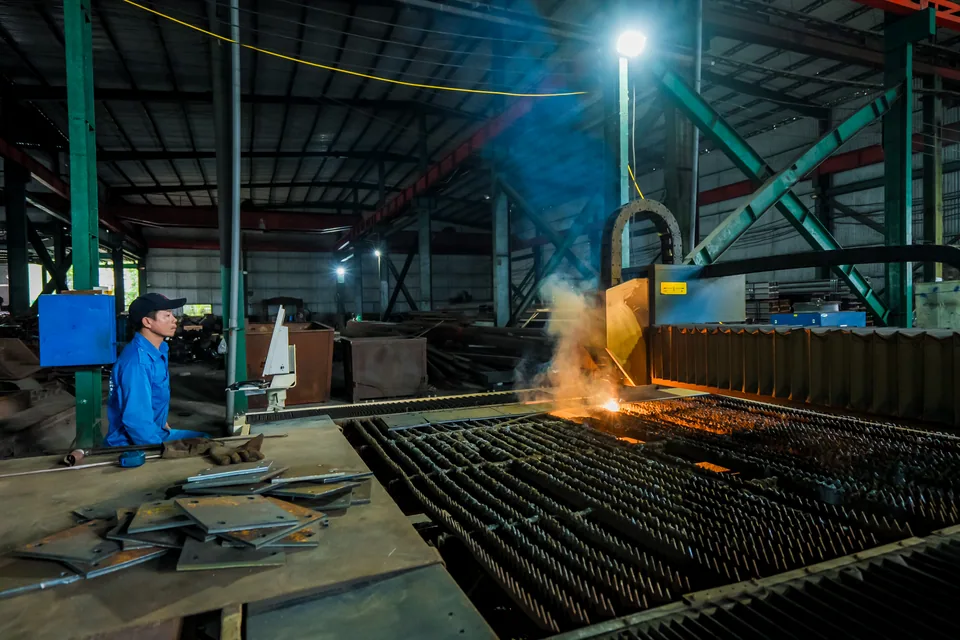
CNC cutting (plasma & laser)
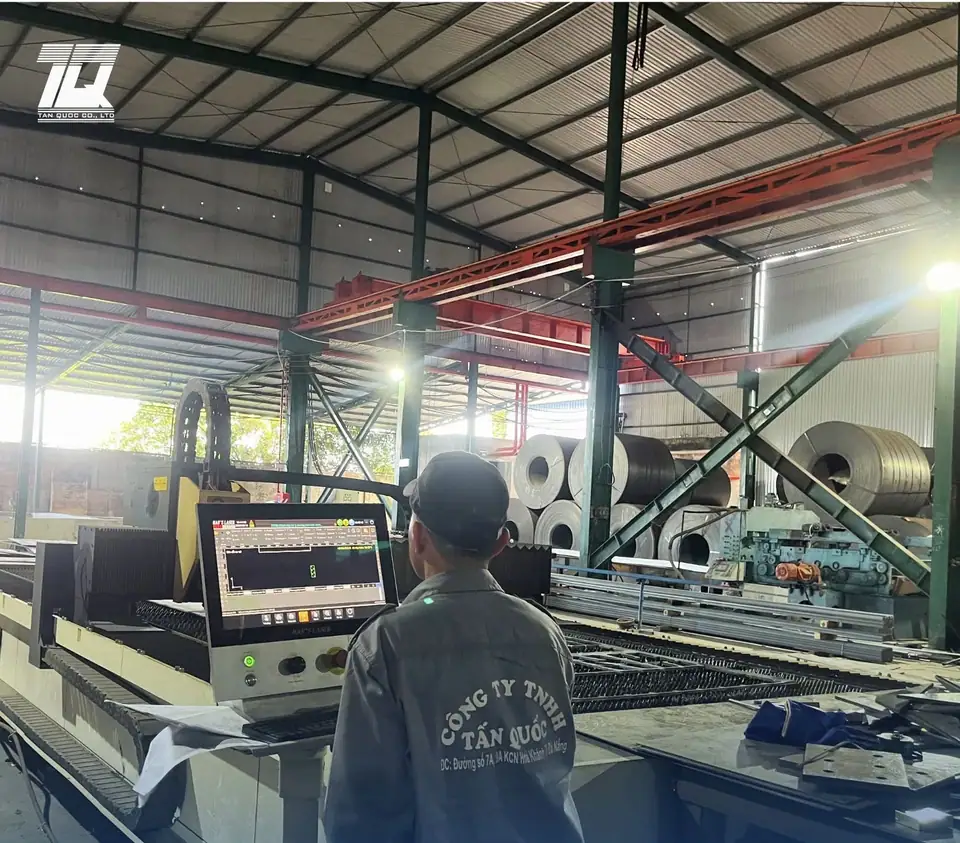
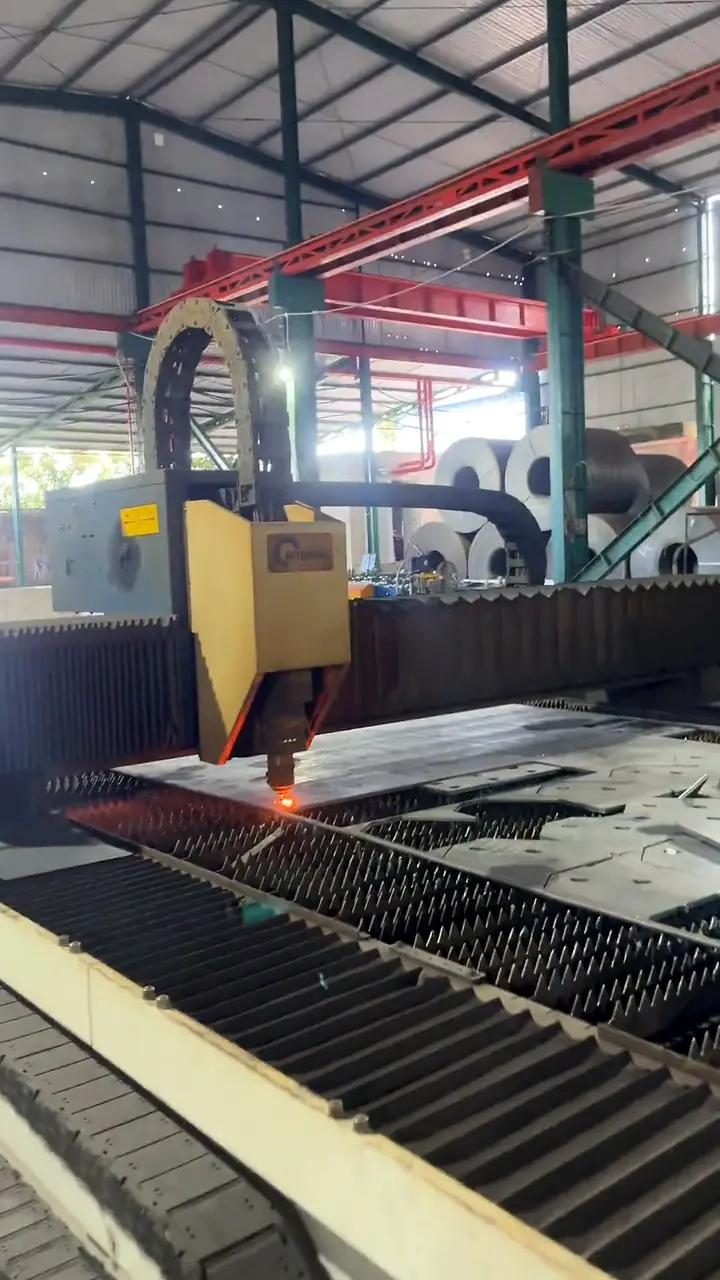
Fibre-laser, plasma and oxy-fuel CNC cutting from CAD files (DWG, DXF): laser delivers clean burr-free edges on thin plate; plasma / oxy-fuel for plate up to 50 mm, tolerance ±1 mm. Includes CNC punching and high-volume hydraulic shearing.
- CNC laser cutting – clean edges, no grinding needed
- CNC plasma / oxy-fuel cutting (≤ 50 mm)
- Punching and stamping
- Hydraulic shearing up to 20 mm
- Band-saw cutting of solid bar and sections
Typical workpieces for the cutting table
Related materials
- Angle (V section) – V25 – V200 sawn to size for bracing, support frames, power towers and handrails
- Square and rectangular hollow sections – cut and punched for building frames, gates, racking and light structures
- Black and galvanized welded pipe – Ø21 – Ø406 cut to length for scaffolding, structures and water supply
- Black flat bar – La14 – La50 cut to size for handrails, door frames and pipe straps
- Rail and crane rail – P11 – P50, QU70 – QU120 cut to the length of factory crane runways
- Larsen sheet piles – U, Z and flat piles 6 – 18 m long, cut to the length required
 04
Bending/forming
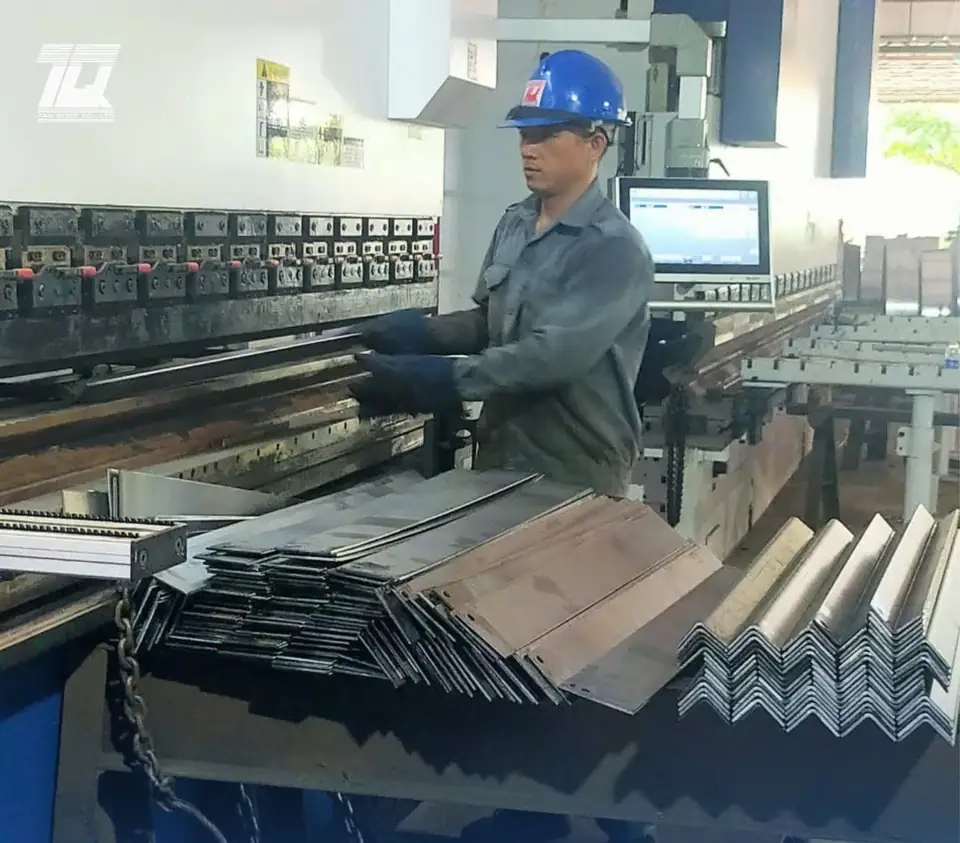
Yawei PBA-500/6200 CNC hydraulic press brake (500-ton force, 6,200 mm bending length) bends and forms steel to drawing angles and radii; press-braking plate into troughs, machine housings, structural members and L / U / Z sections not available as hot-rolled stock.
- Profile bending and forming
- Press-braked L, U, Z sections to drawing
- Cable tray, gutter and purlin forming
- Section and pipe rolling
Sections from the press brake
 05
Structural welding
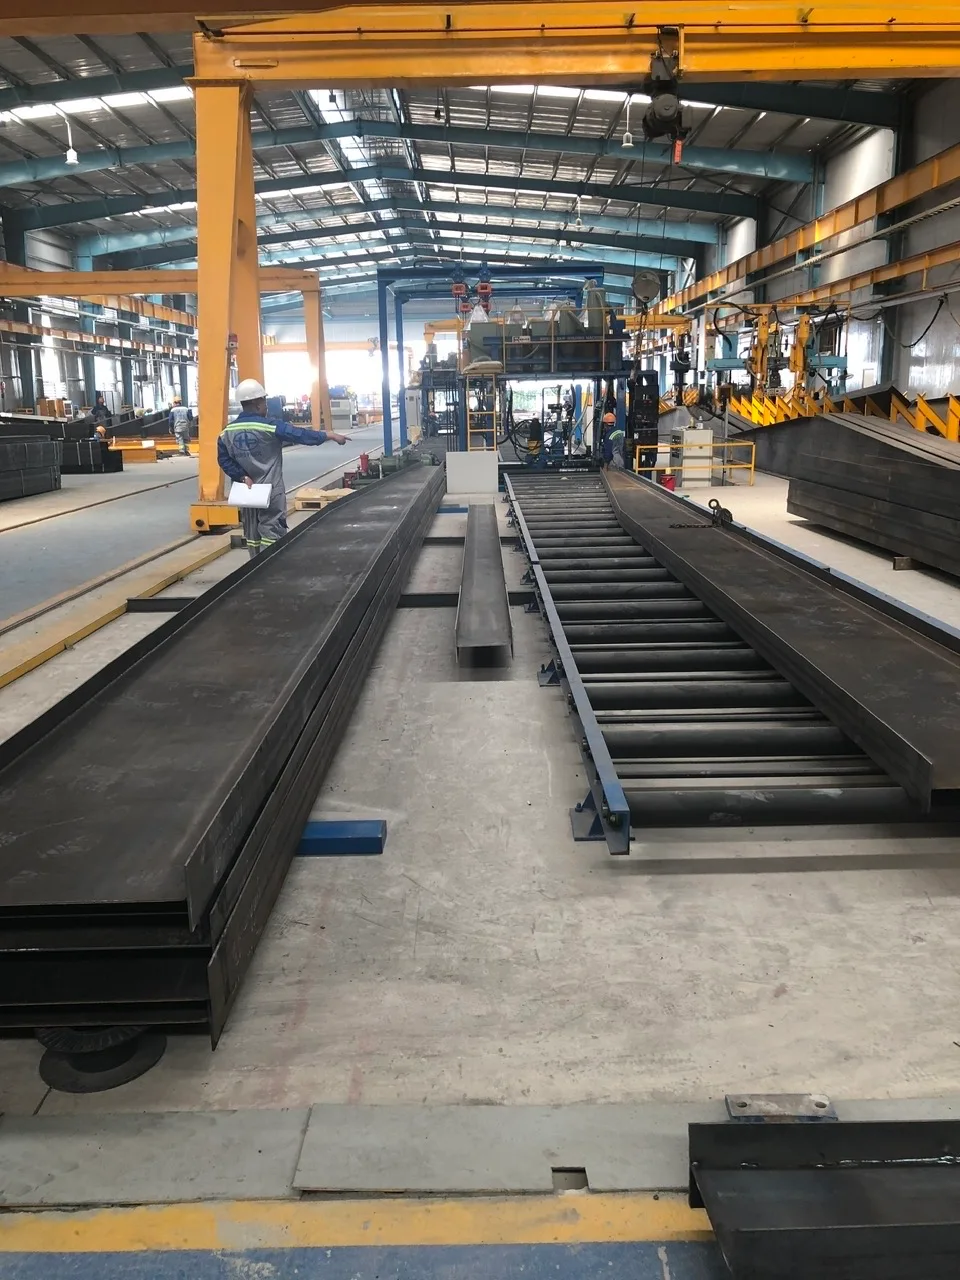
Welding and assembly of columns, beams, trusses and factory frames to design drawings; steel staircases and handrails; matching purlin rolling and deck sheet forming.
- Structural steel welding and assembly
- Steel frames to drawing
- Steel staircases and handrails
- Building and factory structures
- Purlins and deck sheet
Components from the structural shop
Related materials
- H-beam – H100 – H900 for main columns and beams of pre-engineered buildings
- I-beam – I100 – I600 for floor beams and crane girders in bending
- U-channel – U50 – U400 for factory frames, secondary beams and supports
- Steel deck sheet – 50 – 76 mm rib height, replaces slab formwork, laid to beam spans
 06
Surface treatment
Cleaning and protecting components before dispatch: shot-blasting, derusting, anti-corrosion primer and industrial topcoat to the owner's paint specification.
- Shot-blasting to Sa2.5
- Derusting and degreasing
- Anti-rust primer and epoxy coating
- Topcoat to colour code
Products commonly passing through this step
 07
Hot-dip galvanizing
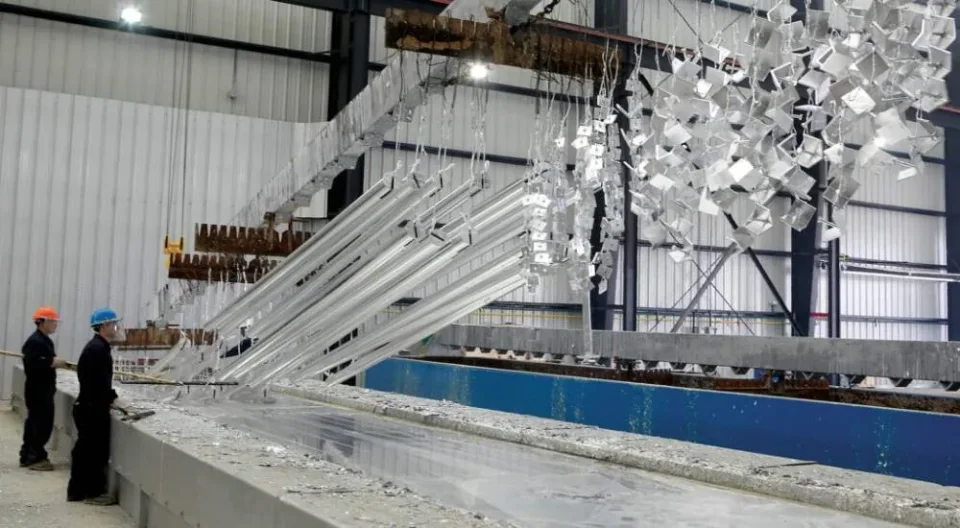
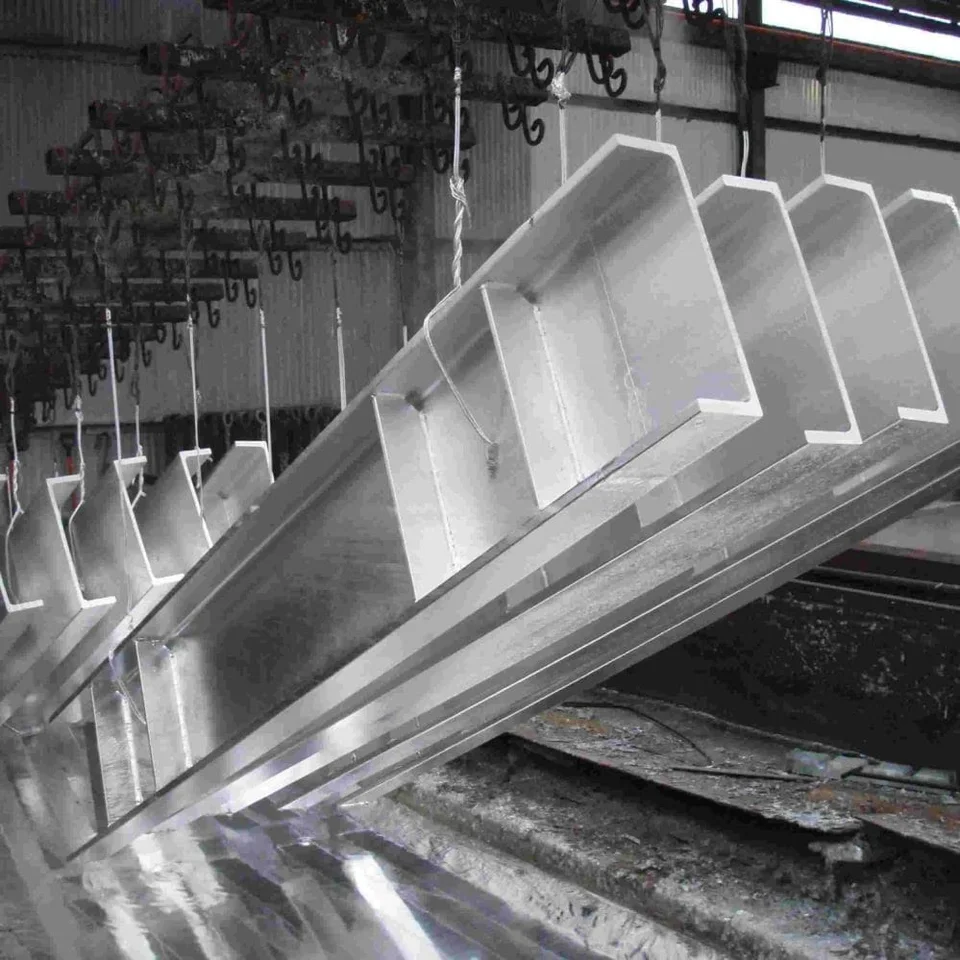
Components are dipped into molten zinc at 450 °C after degreasing, pickling and fluxing: the zinc layer alloys with the steel; minimum coating thickness per TCVN 5408 (ISO 1461) or ASTM A123 – both standards grade values by component thickness, so read the row that matches your component; 30 – 50 year outdoor and coastal protection. Full galvanizing of sections, pipes, purlins, gusset plates, handrails and structures.
- Galvanizing U, I, H, V sections
- Galvanizing pipes, hollow sections, purlins and mesh
- Galvanizing structures, handrails and staircases
- Coating thickness inspection per ASTM A123 / TCVN 5408
Pre-galvanized stock items
Related materials
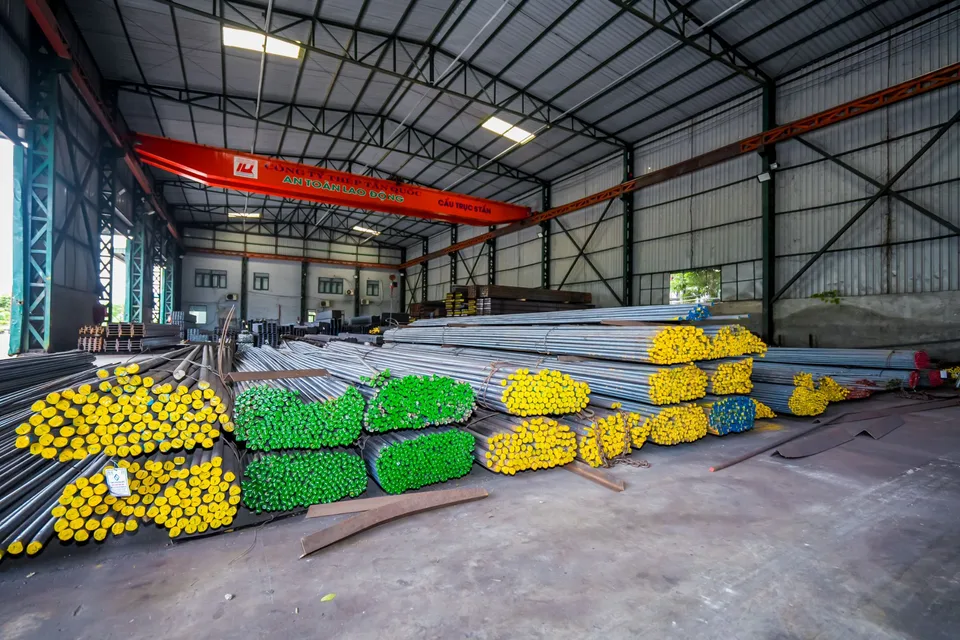
- Galvanized plain round bar – Ø6 – Ø50 hot-dip galvanized for hanger rods, tie bars, anchor bolts and earthing
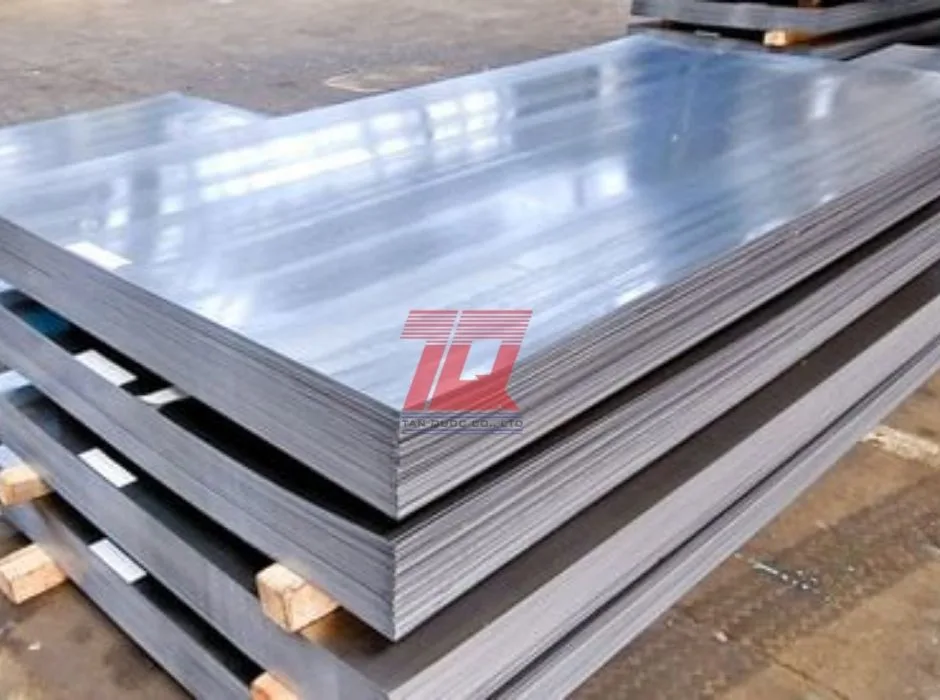
- Galvanized and Galvalume sheet – pre-coated coil or sheet for cladding, ductwork and accessories
- Pre-painted roofing sheet – galvanized or aluminium-zinc base, roll-formed to the ordered length
 08
Other fabrication
Machine parts and specialist components fabricated to drawing using lathe, milling machine, drill press, tapping machine and pipe bending machine.
- Turning and milling
- Steel fabrication to drawing
- Drilling and tapping
- Pipe and plate rolling
Commonly used fabrication blanks
Related materials
- 40Cr / 41Cr4 alloy steel – solid round Ø16 – Ø250 for turned shafts, gears, pins and load-bearing bolts
- SKD11 / P20 tool steel – blanks cut to drawing for cold-stamping dies and plastic injection moulds
- S45C / C45 hexagon bar – S8 – S80 across flats for bolts, nuts, couplings and hex shafts
- Solid square bar – 10×10 – 100×100 mm for dies, guide bars and pins
- Plain round bar – Ø10 – Ø32 for starter bars, stirrups, threaded rods and simple machine parts
- Stainless plate 201 / 304 / 316 – 0.4 – 50 mm for food, chemical and architectural parts
- Round, square and rectangular stainless tube – Ø9.5 – Ø219 with stainless fittings for frames and piping
- Stainless solid bar – round Ø3 – Ø300 for turned shafts, bolts and pins in food and chemical equipment
Steel plate line · six stages
From raw coil to finished product.
Explore the levelling, shearing, CNC cutting or slitting, finished-product inspection and delivery process – every stage photographed at the Hòa Khánh workshop.
-
01Decoiler · 35-ton overhead crane
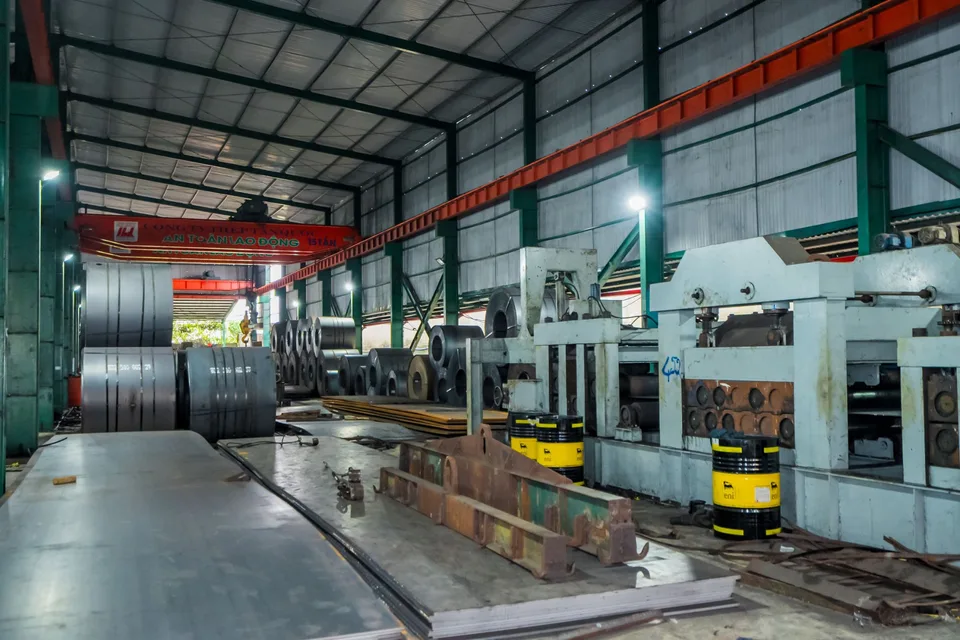
Raw coil loaded into the decoiler
The overhead crane loads a hot-rolled coil onto the decoiler mandrel. From this point on the steel is never lifted again – it travels continuously along the line until it is bundled, so every junction between stages is a potential point of error.
- Thickness range
- 1.2 – 23 mm
- Incoming coil width
- ≤ 1,500 mm
The coil yard is right next to the line, so stock sizes typically start running within 12 hours to 1 day.
-
02CLS-16.6300 hydraulic leveller
Plate levelling
Steel peeled from the coil retains its original curvature. Staggered levelling rolls flex the strip back and forth with decreasing amplitude, releasing residual stress so the plate lies flat without springing back.
- Levelling roll set
- 9 staggered rolls
- After levelling
- No warping
Skip this step and the ±1 mm tolerance of the profiling machine is meaningless – it only cuts relative to the curved blank.
-
03Flying shear on rails · hydraulic shear
Cut-to-length and shearing
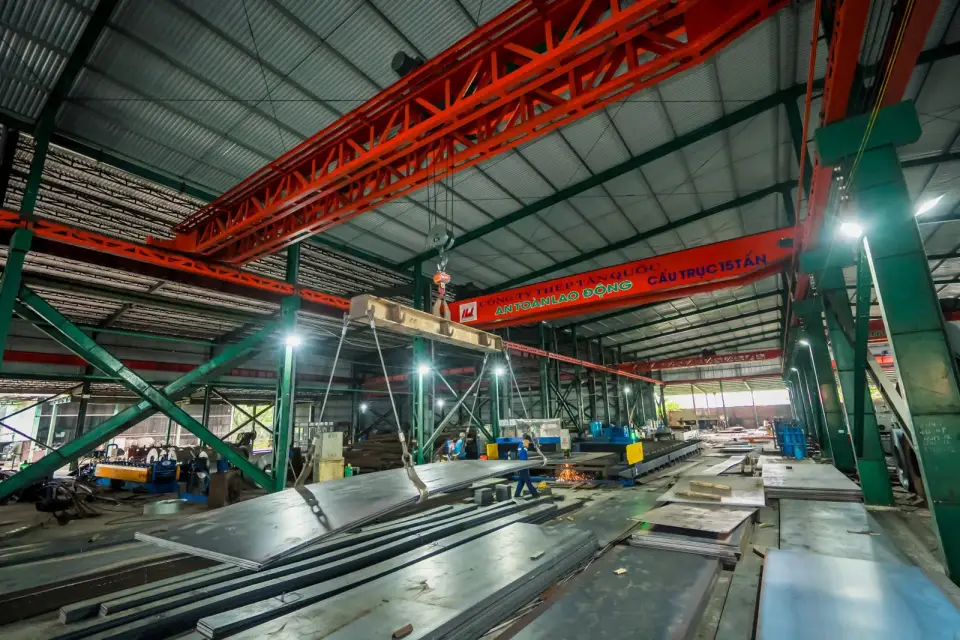
The flying shear chases the moving strip and cuts to the preset length, so the strip does not have to stop at each cut – the edge is square with no end waviness. High-volume orders requiring a straight cut use the hydraulic shear: one clean stroke, no heat generation, so the plate does not re-curve after cutting.
- Cut length
- 1 – 12 m
- Length tolerance
- ±2 mm
Standard sheet size after cutting is 1,500 × 6,000 mm. The hydraulic shear handles up to 20 mm; thicker plate or profiled cuts go to the CNC branch.
-
Branch A · CNC cutting to drawing 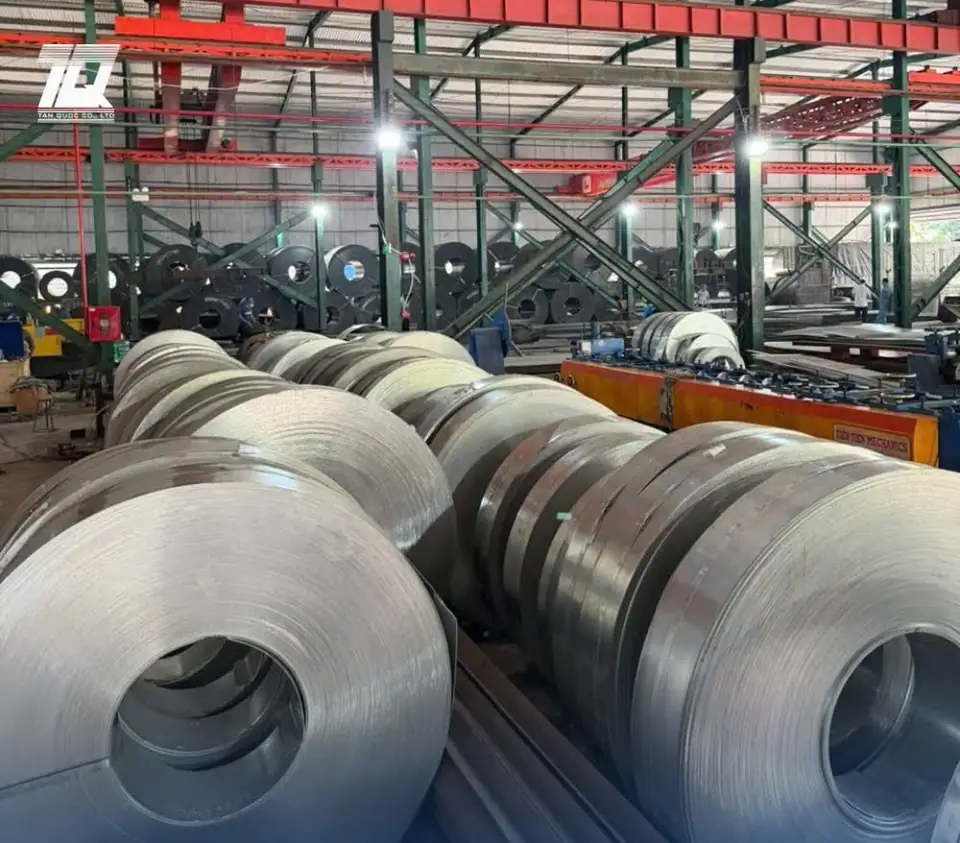
Branch B · Slitting into flat bar 04CNC cutting table · slitting disc blades
Two parallel processing branches
At this point the plate follows the order requirement instead of going through both routes. Parts to drawing go onto the CNC table; flat bar to width goes through the slitting blades. Both branches run in parallel in the same workshop.
Branch A
CNC cutting to drawing
DWG and DXF files loaded directly into the machine – no re-drawing. The cutting head follows the exact drawing profile: gusset plates, flanges, base plates, bolt holes at the correct coordinates.
≤ 50 mm · profile cutting thickness — ±1 mm · cutting tolerance
Branch B
Slitting into flat bar
Disc blades slit the wide strip into multiple flat bar strips to the required width, then bundled to specification.
To order · strip width — 1 – 12 m · bundle length
Parts are nested on the 1,500 × 6,000 mm sheet to minimise scrap. Thin plate requiring clean burr-free edges is cut by fibre laser.
-
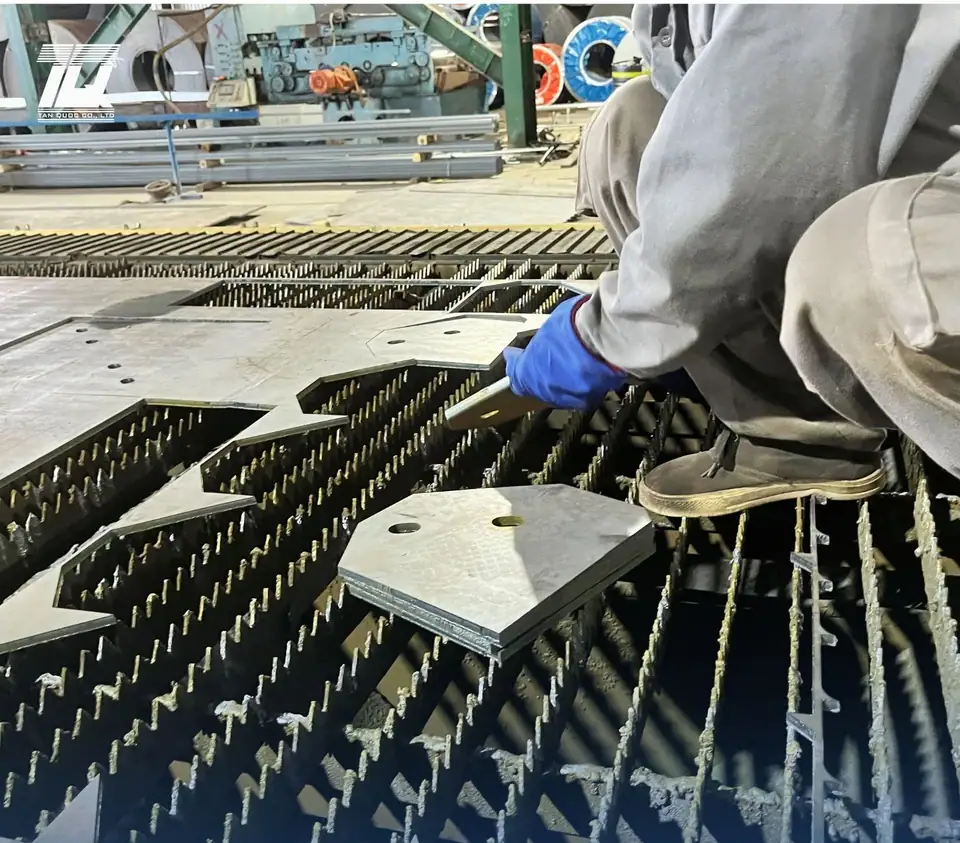
05Re-measurement · drawing check
Finished-product quality inspection
Product from both branches passes through this single stage: each lot is re-measured and checked against the drawing and the order specification. This is the gate that catches mis-cut product before it goes onto the truck.
- Re-measured tolerance
- ±1 – 2 mm
- CO · CQ · MTC
- Mill certificates
Every lot is re-measured before it is bundled and dispatched.
-
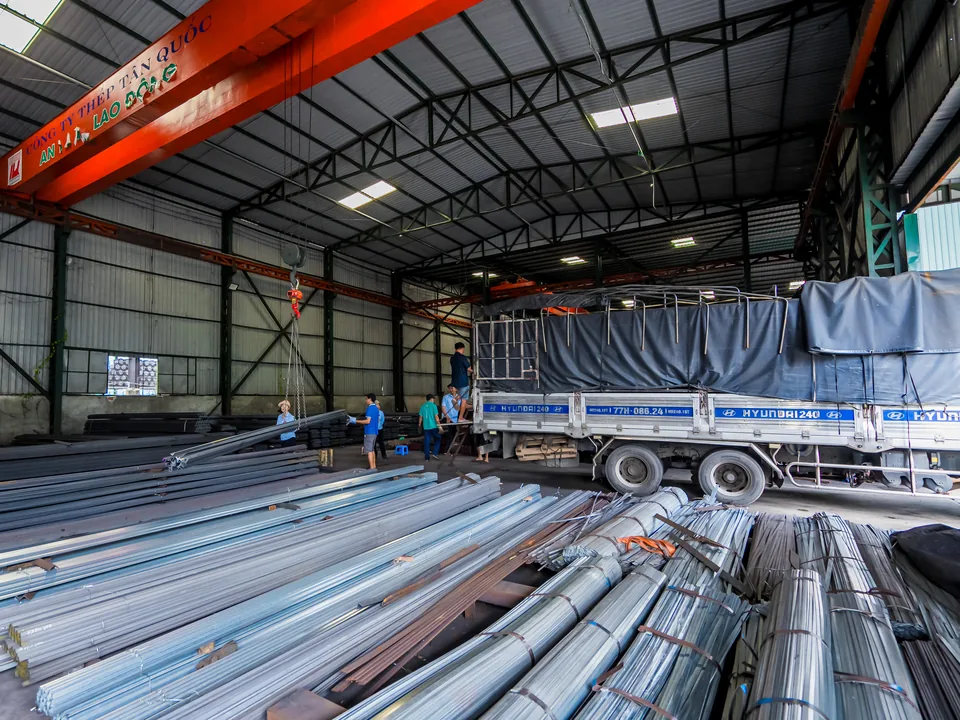
06Overhead crane · transport partner
Bundling & dispatch
Inspected product is stacked, strapped into bundles and lifted onto the truck, together with the mill’s quality certificates (CO, CQ).
- Stock items
- 12 hrs – 1 day
- Delivery area
- 20 provinces
Bundles are delivered through our transport partners, together with their documents.
- 1.2 – 23 mm
- Decoiling thickness
- ≤ 1,500 mm
- Coil width
- 1,500 × 6,000
- Standard sheet size
- ±2 mm
- Length tolerance
Actual finished products
What the steel looks like coming off the line
Photographs from the Hòa Khánh workshop: precision-cut sheets, slit flat bar, CNC-profiled parts, chequered plate and galvanized sheet – neatly bundled before loading.
-
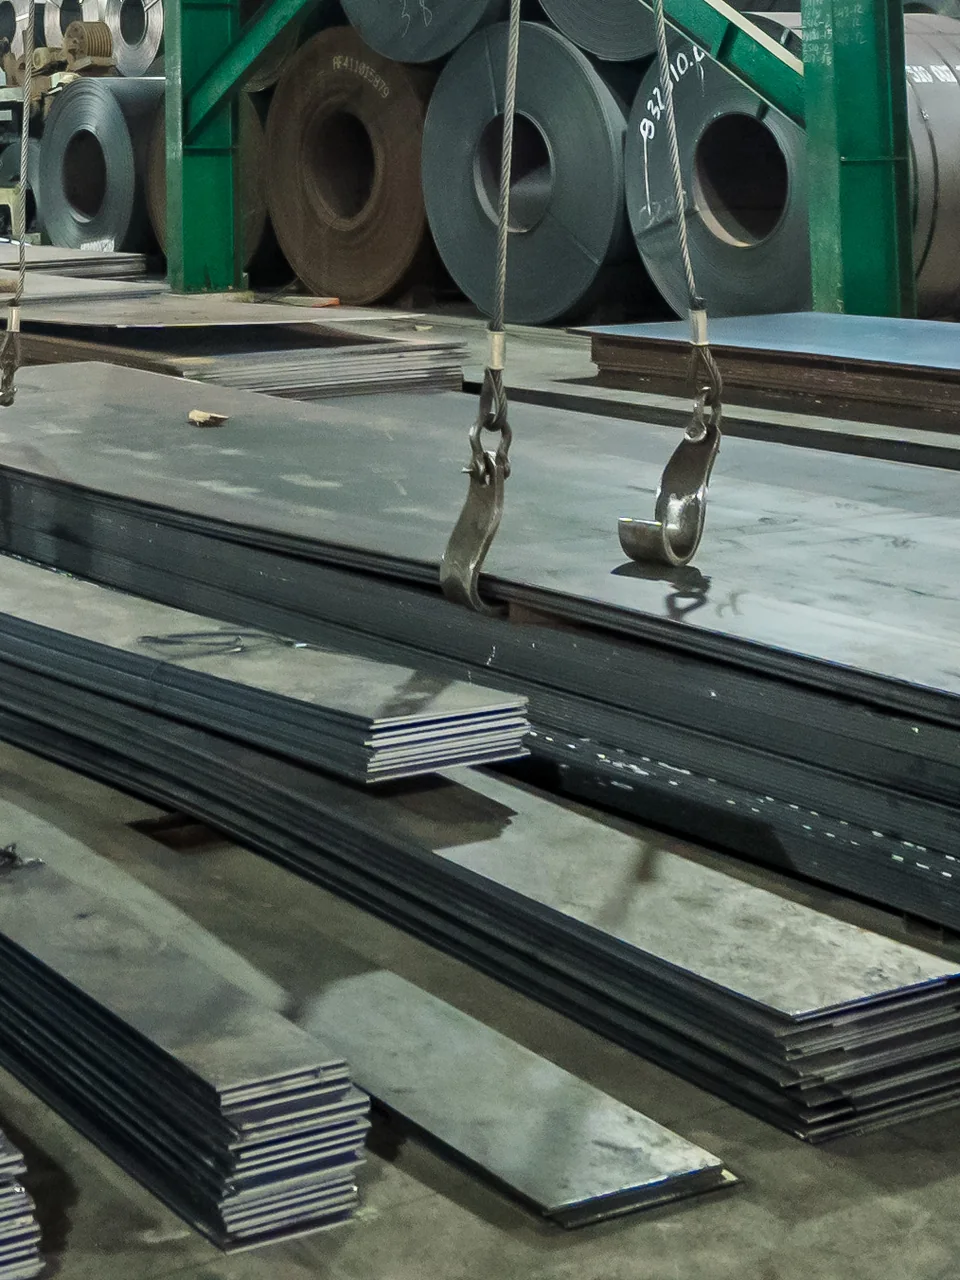 Cut-to-length sheet Standard size 1,500 × 6,000 mm, tolerance ±2 mm01
-
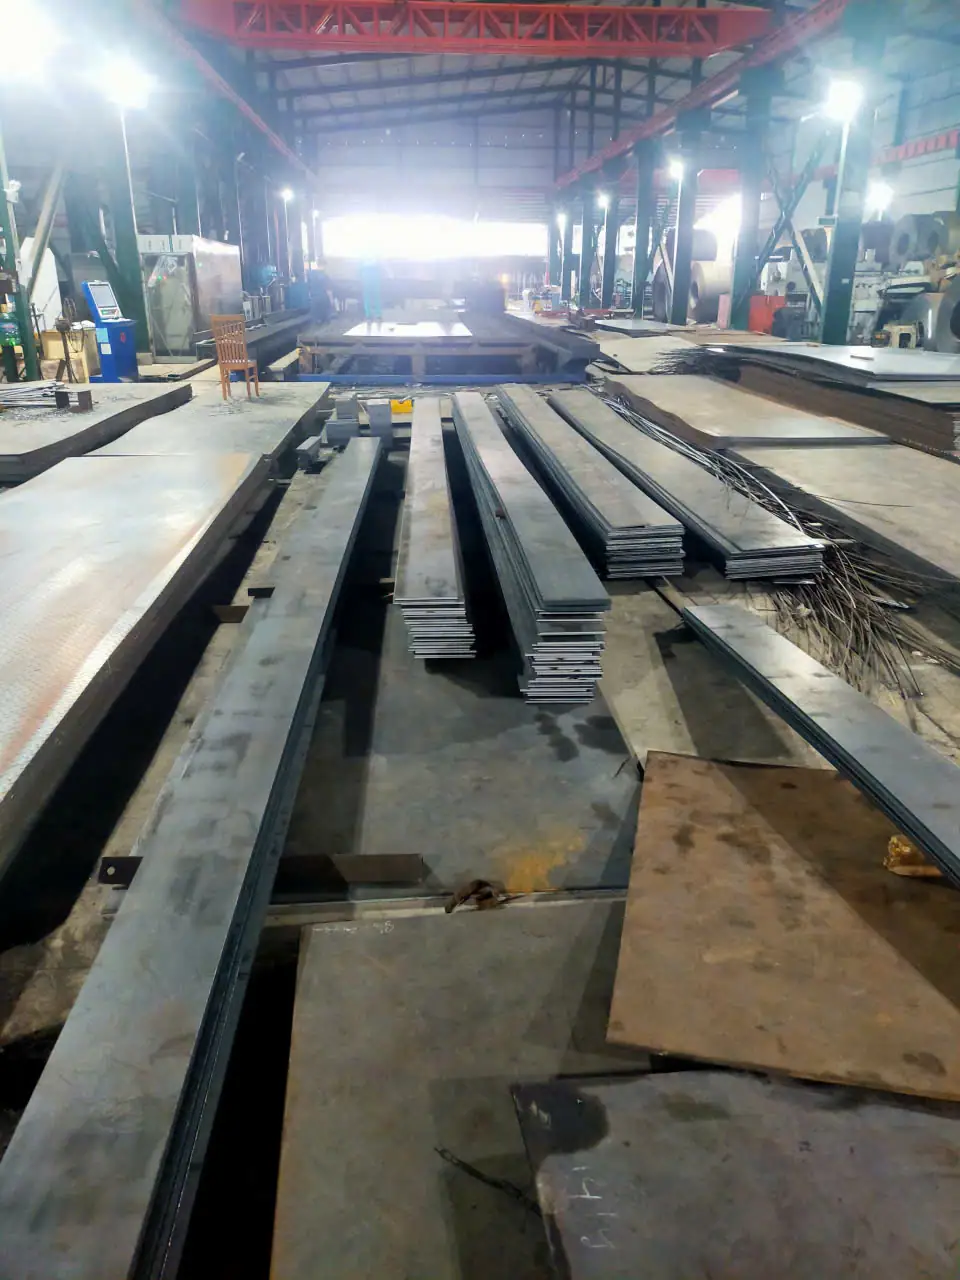 Slit flat bar Slit directly from coil, width to drawing02
-
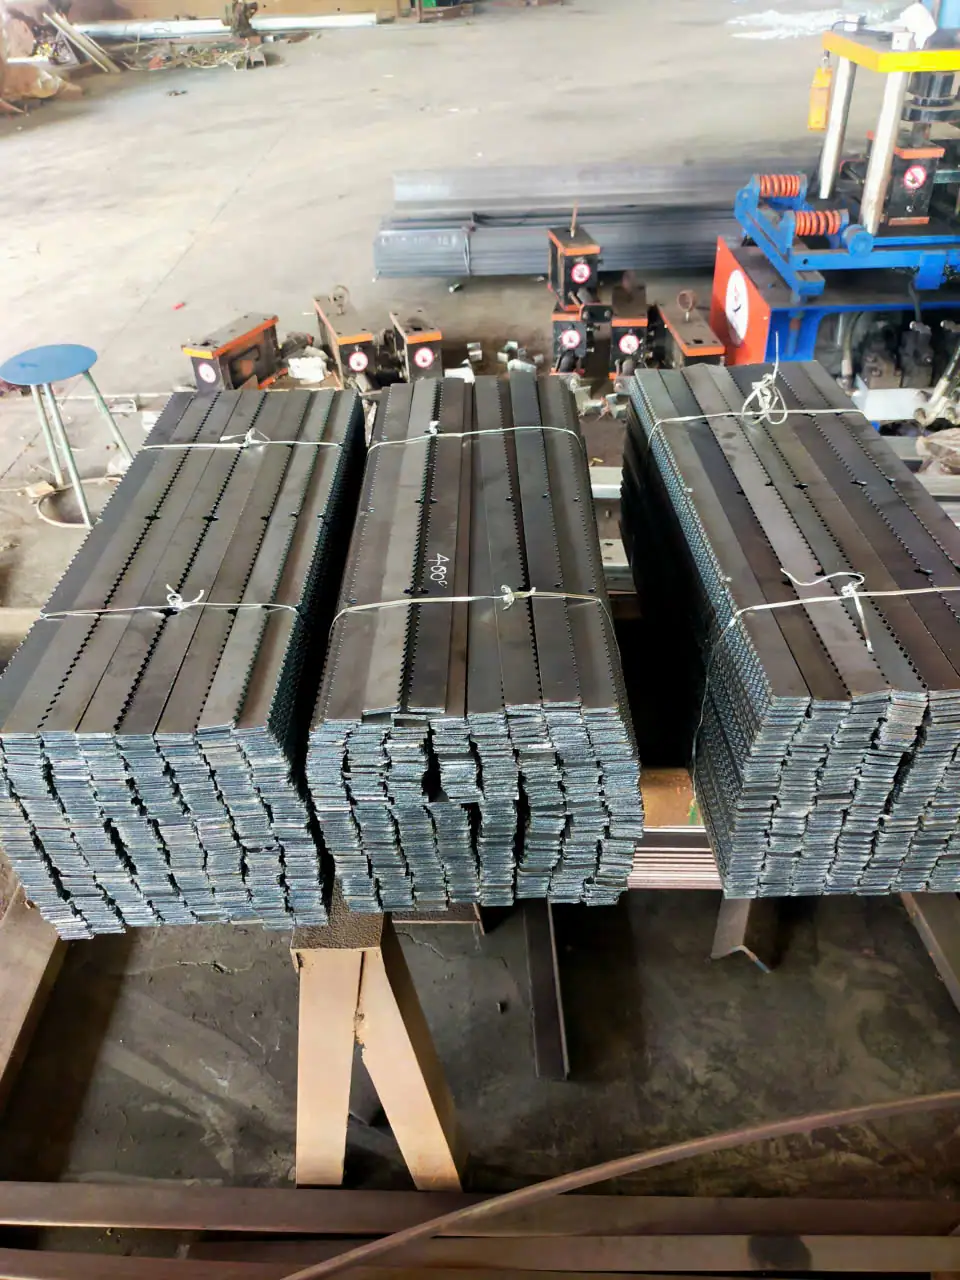 CNC-profiled parts Tooth cutting, punching, profile cutting from CAD file03
-
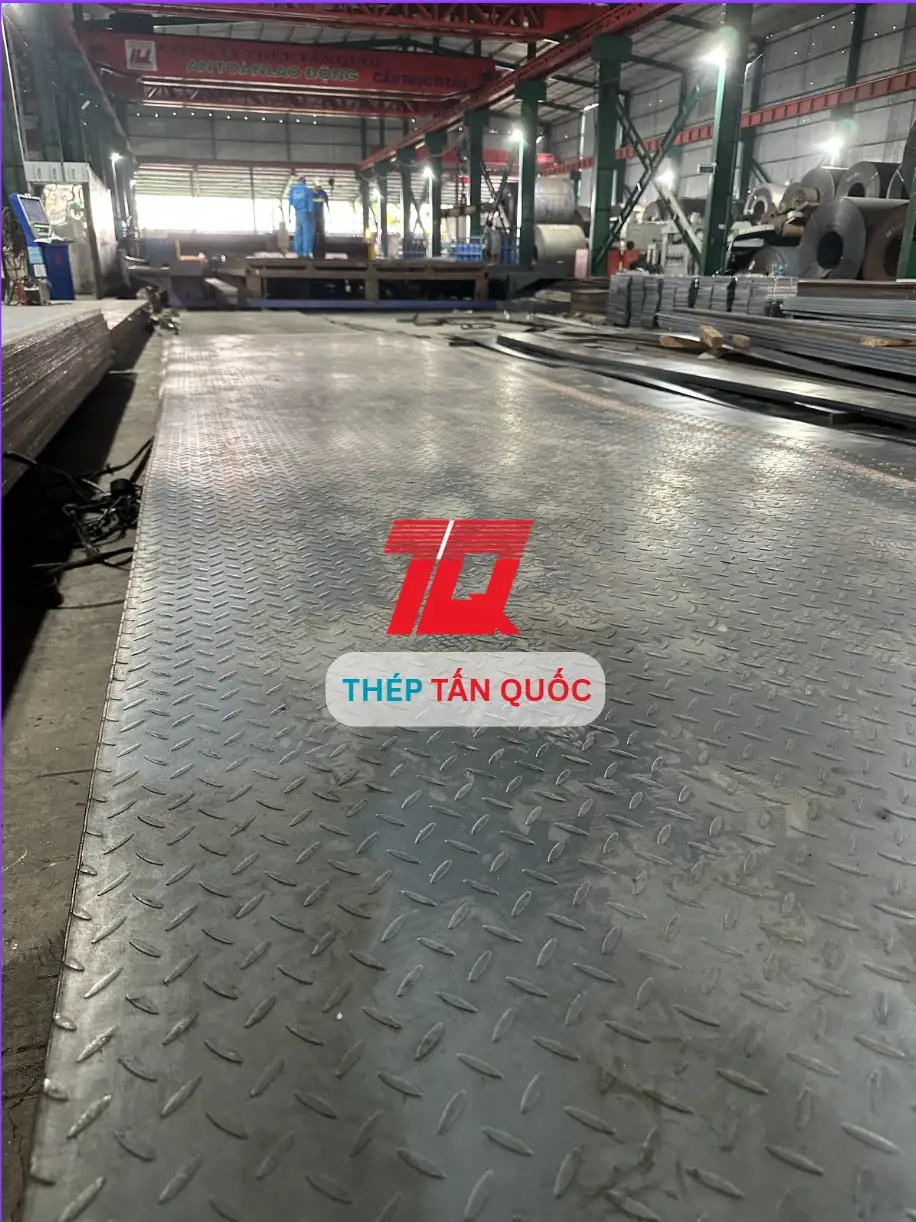 Chequered plate Decoiled from chequered coil, cut to the required length04
-
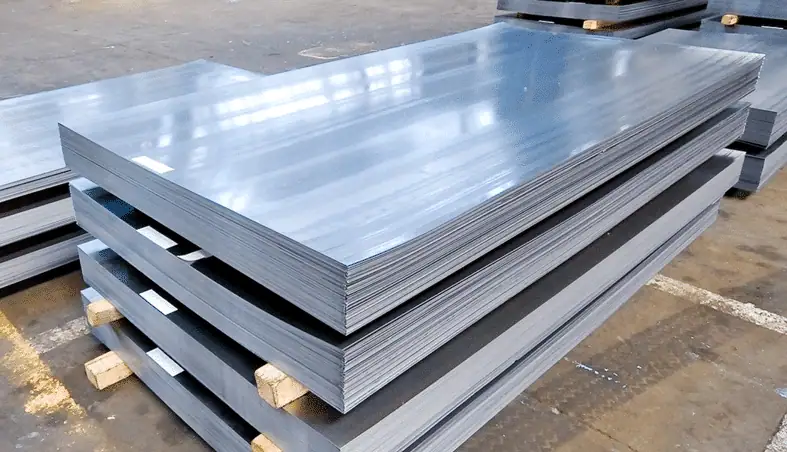 Galvanized sheet Decoiled from GI coil, cut to order05
-
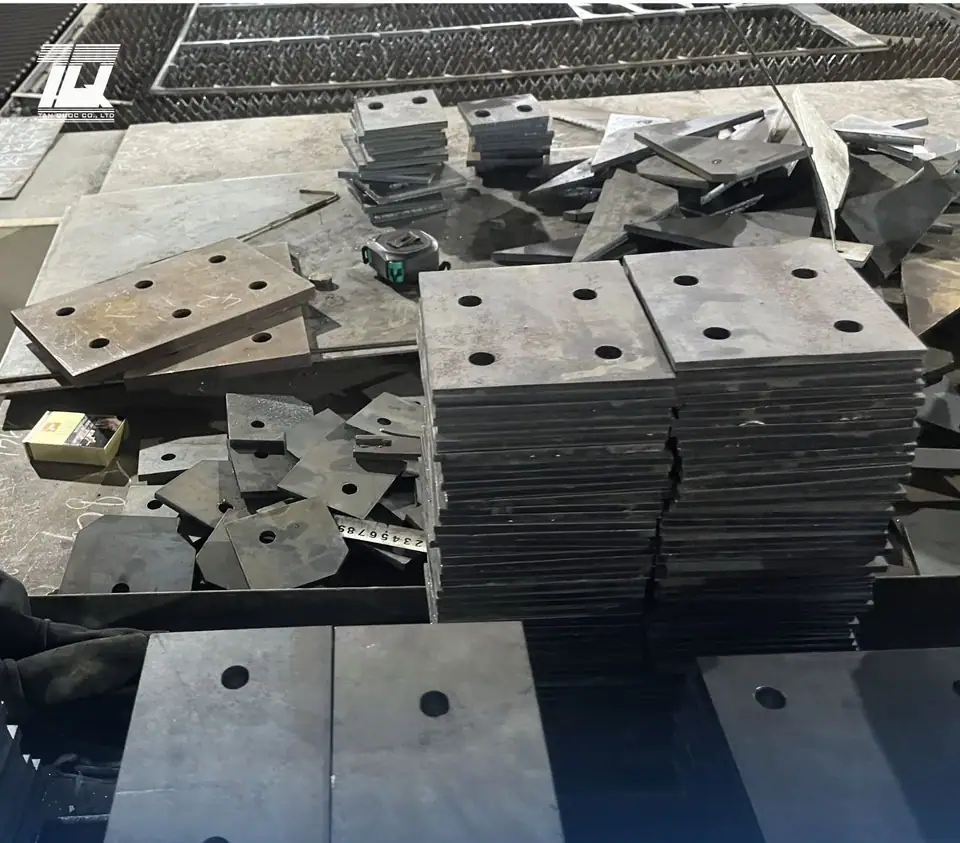 CNC-cut gusset plates Profile cut and drilled from drawing files06
Workshop video
Inside the Tấn Quốc workshop today
Real footage from the Tấn Quốc processing workshop and steel warehouse: the CNC cutting machine at work, workers checking each freshly cut part, the coil store and the overhead crane lifting stock.
- 01CNC cutting to drawing
- 02Every part inspected
- 03Coil store
- 04Overhead crane lifting
The video has no sound. Use the button to pause or play.

Process
4 steps from drawing to finished steel
- 01
Submit your request
Send drawings, specifications or a description via Zalo / email.
- 02
Quote in 2 working hours
Our engineers review, advise on optimal materials and send a quotation.
- 03
Processing
The plant processes each order to schedule, inspecting dimensions lot by lot.
- 04
Bundling & dispatch
Inspected product is bundled and craned onto the truck.
Capability
Custom processing
Cutting & welding, forming, drilling & punching, straightening, surface treatment: a full turnkey service to drawing at the Hòa Khánh plant – steel leaves the plant ready for erection.
- Tolerance ±1 mm
Cutting & welding
CNC plasma / oxy-fuel cutting from DWG / DXF files, fibre-laser cutting of thin plate, band-saw cutting of solid bar; automated submerged-arc welding of built-up beams and columns.
- 500 ton · 6,200 mm
Forming
Bending and forming on a Yawei PBA-500/6200 CNC press brake – 500-ton force, 6,200 mm bending length.
-
 To drawing
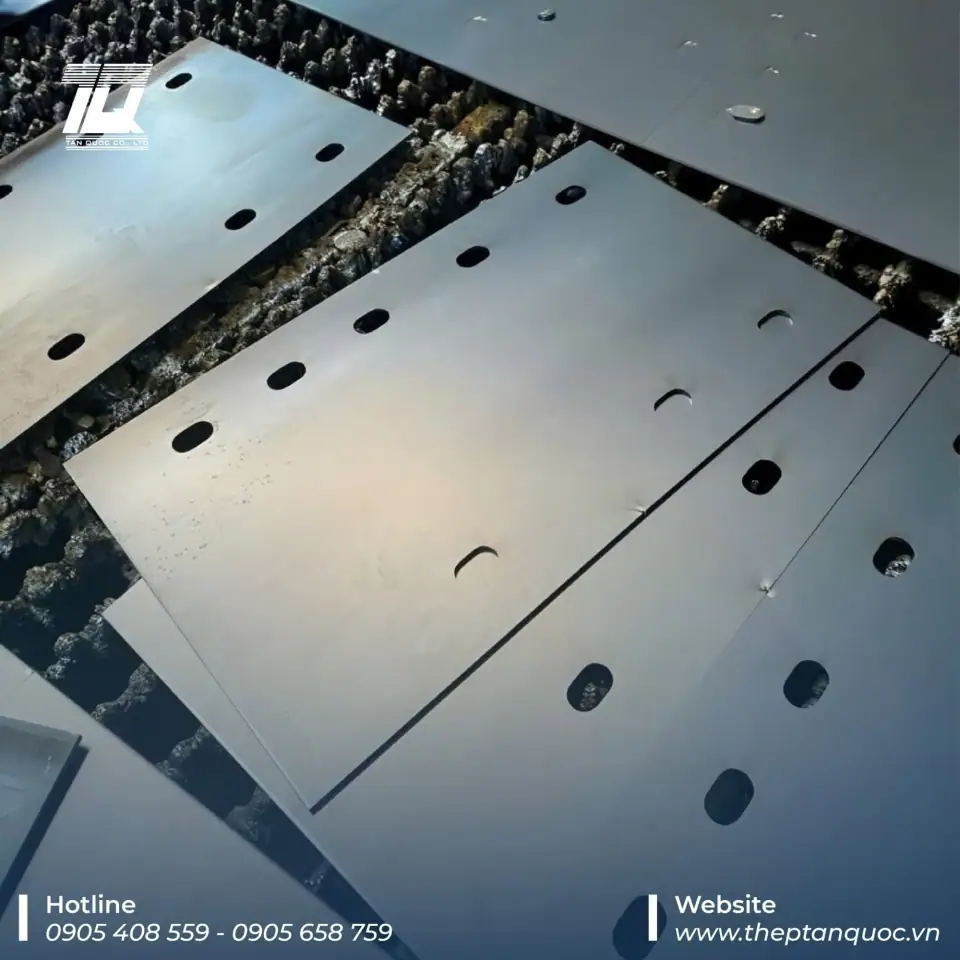
Drilling & punching
CNC bolt-hole drilling, round and oval hole punching to drawing, accurate hole pitch.
- No warping
Straightening
Hydraulic straightener and plate leveller bring sections and plate back to true, eliminating warping.
-
 Galvanizing per TCVN 5408
Surface treatment
Shot-blasting to Sa2.5, anti-rust primer and topcoat, or hot-dip galvanizing for outdoor and coastal structures.
Projects supplied
CNC cutting items in the project file
The project pages below list CNC cutting to drawing among the materials Tan Quoc supplied. Open each page to see the steel types and specific items for that project.
- Hue · Da Nang
La Son – Tuy Loan Expressway
U, I, V sections · plate and gusset plate · hot-rolled coil
- Da Nang · Quang Nam · Quang Ngai
Da Nang – Quang Ngai Expressway
Plate and gusset plate for connection details
- Ha Tinh
Vung Ang 1 Thermal Power Plant
Heavy plate and gusset plate for foundations and load-bearing structures
- Thanh Hoa
Nghi Son Oil Refinery and Petrochemical Plant
Heavy plate and gusset plate for industrial fabrication
- Da Nang
Song Thu Shipyard
Plate and gusset plate in multiple thicknesses for marine environments
- Quang Binh
Quang Trach Power Centre
Heavy plate for equipment foundations, gusset plates and support structures
See the full list of landmark projects.
Answers
Processing FAQ
Plant capability, tolerances, drawing formats and how to request a quotation.
Processing
What processing services does Tan Quoc Steel offer?
Coil slitting and cut-to-length, fibre laser cutting, CNC plasma and oxy-fuel cutting from CAD files, steel straightening, press-brake forming, sawing solid round bar to size, welding of beams and steel structures, and hot-dip galvanizing.
What coil thickness and width can the cut-to-length line handle?
The cut-to-length line at the Hòa Khánh Industrial Park plant accepts hot-rolled coil from 1.2 to 23 mm thick and up to 1,500 mm wide.
What are the cutting tolerances, and are goods checked before dispatch?
It depends on the process: cut-to-length on the coil line holds ±2 mm, while CNC plasma / oxy-fuel cutting and band-sawing of solid round bar and sections hold ±1 mm. Standard plate size is 1,500 × 6,000 mm. Before bundling, every lot is re-measured before it leaves the warehouse.
Which drawing formats do you accept, and how heavy a component can the plant lift?
The plant accepts DWG, DXF and PDF drawings for CNC cutting to the exact profile. The overhead cranes at the plant and warehouse lift up to 35 tonnes.
Quotes & ordering
How long does it take to get a steel quotation from Tan Quoc Steel?
Our sales team responds within 2 working hours. You can call the hotline 0393 295 305, message us on Zalo or use the form on the Contact page. For processing orders, the engineering team reviews your drawings and advises on material optimisation before the quotation is sent.
What information do you need for a quick quotation?
Steel type and grade, specifications, quantity required, delivery location and the date you need the goods. For processing orders, please attach your drawings – the plant accepts DWG, DXF and PDF files.
Can I inspect the goods in person before ordering?
Yes. The warehouse and plant are open Mon – Sat: 7:30 – 17:30. Head office: 267 Hoàng Diệu, Hải Châu Ward, Đà Nẵng City; processing plant: Lot 6, Road 9A, Hòa Khánh Industrial Park, Liên Chiểu Ward, Đà Nẵng City; warehouse: Lot Q, Road 7A, Hòa Khánh Industrial Park, Liên Chiểu Ward, Đà Nẵng City.
Is there a minimum order quantity?
There is no minimum order. We accept anything from a few bars or loose plates up to orders of hundreds of tonnes for projects.
What are the payment terms? Do you offer credit?
Payment terms are assessed for each customer. Customers with an established trading history and good credit may be considered for credit terms. For new customers or first orders, our sales team states the specific terms together with the quotation.
Quote in 2 working hours
Send drawings, receive a processing quote in 2 working hours
Call 0338 636 025 or email info@theptanquoc.vn. We accept DWG, DXF and PDF files, or a photo of a hand sketch.